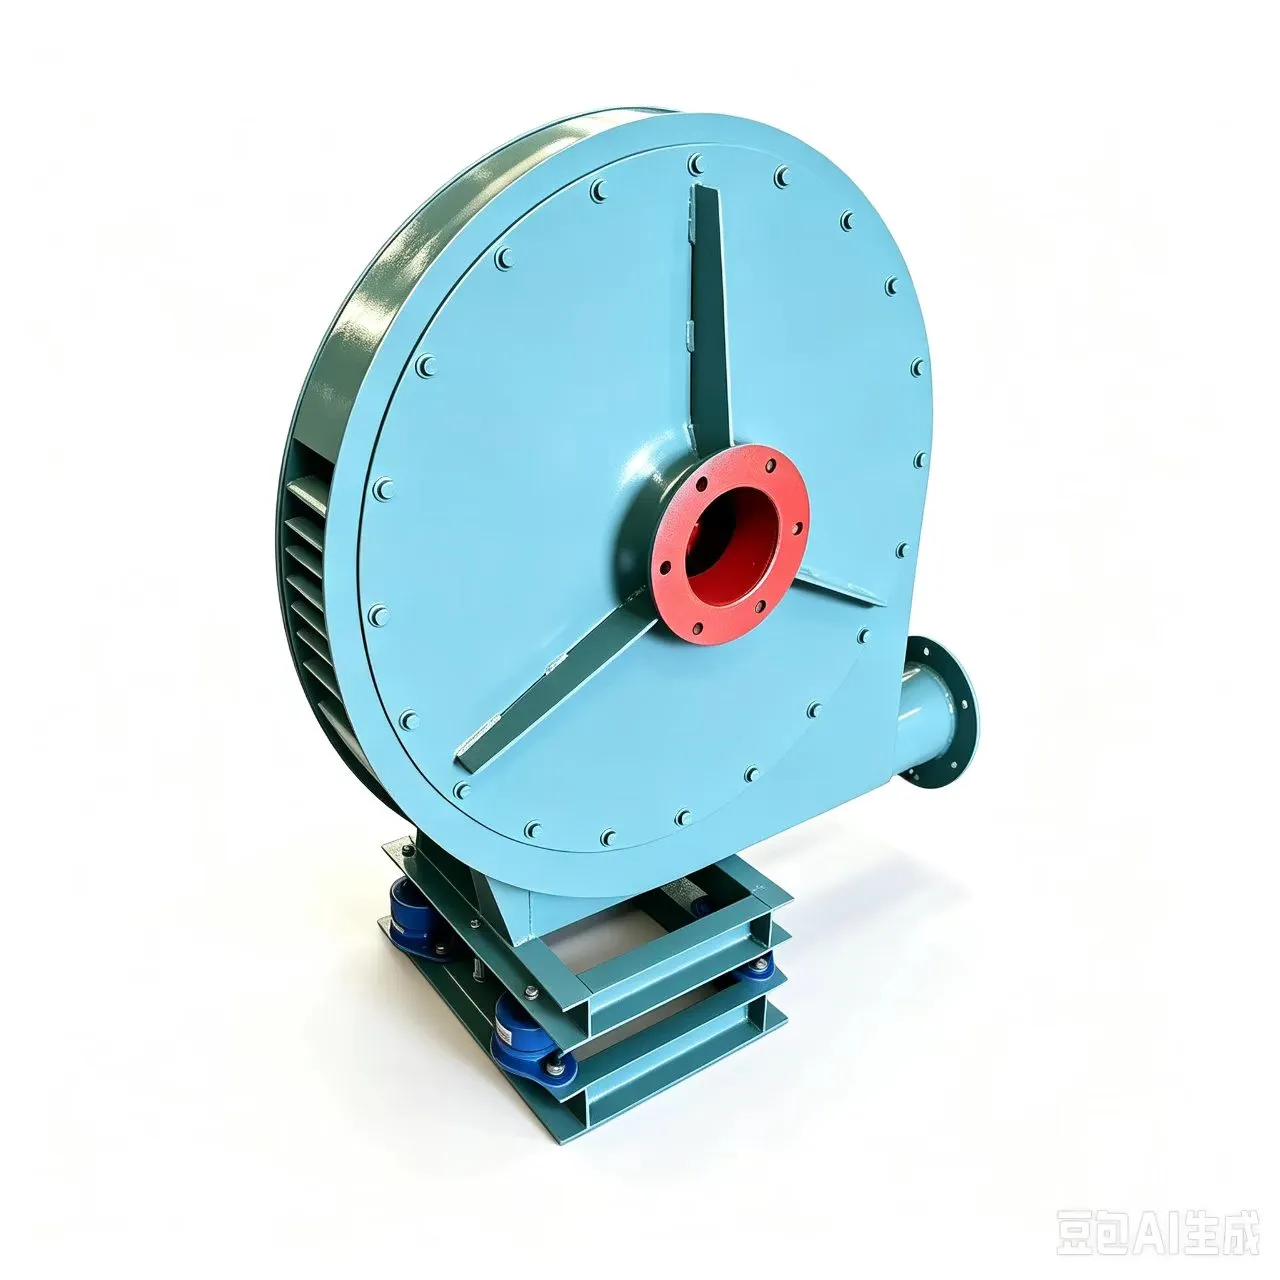
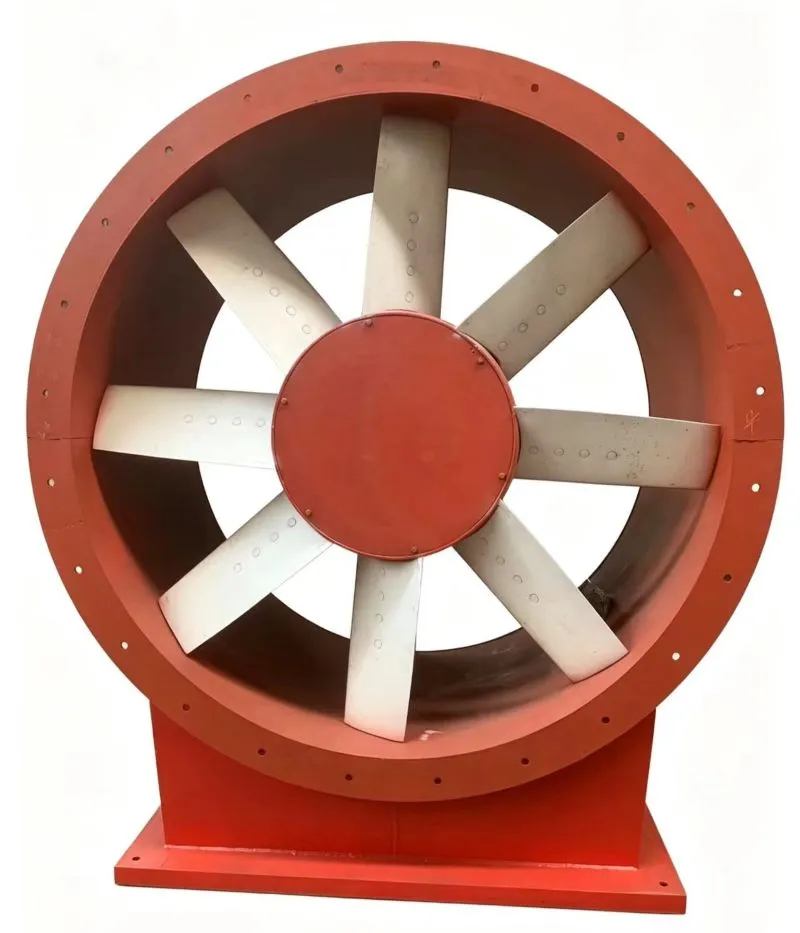
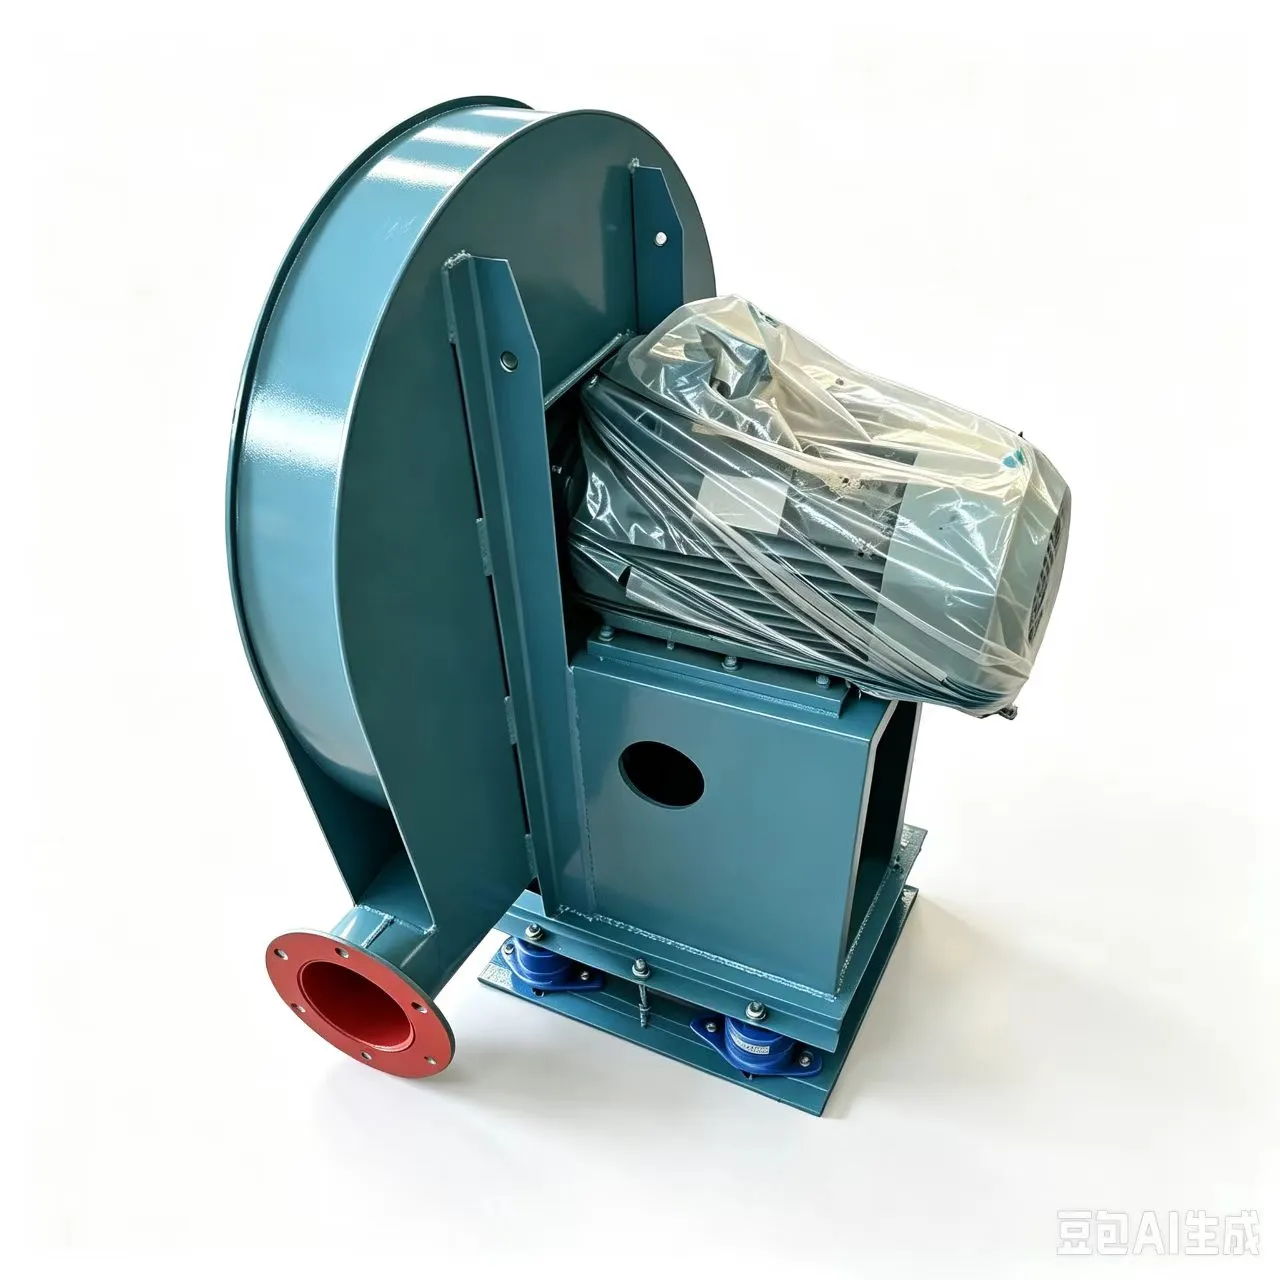
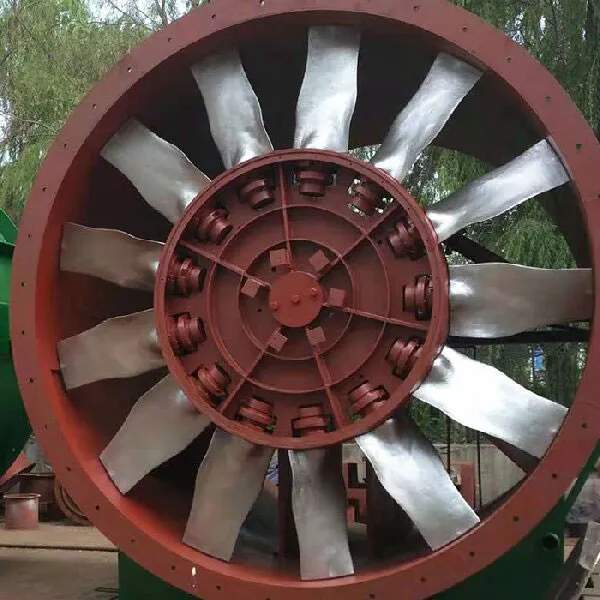
An explosion-proof variable frequency motor is a specialized industrial drive system designed to operate safely in hazardous environments containing flammable gases, vapors, or dust. By integrating robust explosion-proof enclosures with precise frequency control technology, these motors prevent ignition sources while allowing for adjustable speed and torque. This combination ensures operational safety in high-risk sectors like mining, oil and gas, and chemical processing, while significantly improving energy efficiency and process control compared to fixed-speed alternatives.
What Is an Explosion-Proof Variable Frequency Motor?
An explosion-proof variable frequency motor combines two critical engineering concepts: intrinsic safety in hazardous areas and advanced speed control. Unlike standard motors, these units are built to contain any internal explosion, preventing it from igniting the surrounding atmosphere. When paired with a Variable Frequency Drive (VFD), the motor can adjust its rotational speed by varying the input frequency and voltage.
This integration is not merely about adding a drive to a sealed motor. It requires careful thermal management and electrical insulation design. The VFD generates harmonic currents that can cause additional heating in the motor windings. Therefore, an authentic explosion-proof VFD motor must be rated for inverter-duty operation, ensuring that the insulation system can withstand high-voltage spikes and that the cooling system remains effective even at low speeds.
Core Components and Working Principle
The system consists of three main entities: the explosion-proof motor body, the variable frequency drive, and the specialized cabling. The motor housing is typically cast from heavy-duty aluminum or steel, with flame paths designed to cool escaping gases below their ignition temperature. Inside, the rotor and stator are optimized for variable speed operation.
- Explosion-Proof Enclosure: Prevents internal sparks or heat from contacting external hazardous substances.
- Inverter-Duty Insulation: Protects windings from voltage spikes generated by the VFD’s PWM (Pulse Width Modulation) output.
- Enhanced Cooling System: Often includes independent fans or forced ventilation to maintain temperature limits during low-speed operation.
- Variable Frequency Drive (VFD): Converts fixed grid power into variable frequency power to control motor speed and torque.
Why Use Variable Frequency Control in Hazardous Areas?
In industries such as coal mining and petrochemical processing, safety is the primary concern. However, operational efficiency is equally critical. Traditional explosion-proof motors often run at fixed speeds, controlled by mechanical dampers or valves. This method wastes energy and offers poor process precision. Integrating variable frequency technology addresses these challenges directly.
Energy Efficiency and Cost Reduction
Fan and pump applications follow the affinity laws, where power consumption is proportional to the cube of the speed. By reducing the motor speed by just 20%, energy consumption can drop by nearly 50%. In large-scale industrial facilities, this translates to significant operational cost savings. An explosion-proof variable frequency motor allows precise matching of motor output to process demand, eliminating energy waste associated with throttling devices.
Precise Process Control
Many hazardous processes require strict control over airflow, pressure, or flow rate. For example, in a chemical reactor, maintaining a specific ventilation rate is crucial for safety and product quality. VFDs enable smooth acceleration and deceleration, reducing mechanical stress on belts, bearings, and couplings. This soft-start capability also prevents sudden current surges that could trip protective systems or cause voltage dips in the plant’s electrical network.
Extended Equipment Lifespan
Mechanical wear is a major cause of downtime in industrial settings. By eliminating hard starts and stops, variable frequency control reduces shock loads on the motor shaft and connected machinery. This results in longer bearing life, reduced maintenance frequency, and higher overall reliability. For explosion-proof equipment, which is often difficult and expensive to service due to safety protocols, extended maintenance intervals are a significant advantage.
Key Applications Across Industries
The versatility of explosion-proof variable frequency motors makes them essential in various high-risk sectors. Understanding the specific environmental requirements of each industry helps in selecting the right protection level and motor specifications.
Mining and Coal Processing
Underground mines present some of the most challenging environments, with risks of methane gas and coal dust explosions. Ventilation systems in mines must be reliable and adjustable to respond to changing gas levels. Axial flow fans driven by explosion-proof VFD motors provide critical airflow control. These systems must withstand harsh conditions, including high humidity, dust, and physical impact.
Oil and Gas Exploration
From offshore platforms to refineries, the presence of hydrocarbon vapors requires strict adherence to safety standards. Motors used in pumping stations, compressors, and ventilation systems must meet rigorous certification standards such as ATEX or IECEx. Variable speed control allows for precise pressure management in pipelines and efficient operation of centrifugal compressors, which are sensitive to speed variations.
Chemical and Pharmaceutical Manufacturing
Chemical plants often handle volatile solvents and reactive substances. Explosion-proof motors drive mixers, agitators, and exhaust fans in these facilities. The ability to precisely control mixing speeds via VFDs ensures consistent product quality while maintaining safety. Additionally, corrosion-resistant variants are often required to withstand aggressive chemical atmospheres.
Metallurgy and Boiler Systems
In metallurgical processes, high temperatures and combustible dust are common. Induced draft fans in boiler systems require precise speed control to maintain optimal combustion efficiency and emissions compliance. Explosion-proof variable frequency motors ensure safe operation in these high-temperature, high-dust environments, providing stable airflow control for efficient fuel burning.
Zibo Hongcheng Fans: Expertise in Hazardous Environment Solutions
When sourcing critical safety equipment, the manufacturer’s experience and production capabilities are paramount. Zibo Hongcheng Fans, located within the Zibo Blower Industrial Park in Shandong Province, China, has established itself as a reliable partner for industrial ventilation and motor solutions. Established in 2020 by founders with over 20 years of experience in the blower industry, the company leverages deep technical knowledge to deliver high-performance products.
Spanning 9,000 square meters, our facility employs over 30 skilled staff members dedicated to quality and innovation. While our core expertise lies in mining axial flow fans, centrifugal ventilators, and stainless steel corrosion-resistant fans, we understand that the motor is the heart of any ventilation system. We offer more than 50 series and over 600 specifications, ensuring that our ventilation solutions are perfectly matched with robust drive systems.
Our production process is equipped with comprehensive supporting equipment and adheres to a sound quality management system. Every product undergoes strict quality control to ensure all technical indicators meet national standards. For clients requiring specialized solutions, we provide customized production services. Whether you need a specific explosion-proof rating, a unique mounting configuration, or integration with existing control systems, our team can tailor solutions to meet personalized demands across mines, oil fields, chemical plants, and other hazardous industries.
How to Choose the Right Explosion-Proof VFD Motor
Selecting the correct motor involves more than just matching horsepower. Engineers must consider environmental classifications, thermal performance, and compatibility with the drive system. Making the wrong choice can lead to premature failure or, worse, safety incidents.
1. Identify the Hazardous Area Classification
The first step is determining the zone classification. Is the area Zone 1 (likely to have explosive atmosphere) or Zone 2 (unlikely but possible)? Is the hazard gas (Group IIA, IIB, IIC) or dust (IIIA, IIIB, IIIC)? The motor’s protection level (e.g., Ex d, Ex e, Ex t) must match or exceed the requirements of the installation site. For coal mines, specific mining certifications (like MA in China) are mandatory.
2. Verify Inverter-Duty Rating
Not all explosion-proof motors are suitable for VFD use. Standard motors may suffer from insulation breakdown due to voltage reflections. Ensure the motor is labeled as “Inverter Duty” or “VFD Ready.” Key features to look for include:
- Class F or H Insulation: Higher thermal tolerance for additional heating.
- Shaft Grounding Rings: To prevent bearing damage from stray currents.
- Filtered Output Compatibility: Ability to work with dV/dt filters if long cable runs are involved.
3. Assess Cooling Requirements at Low Speeds
Standard self-cooled motors rely on a shaft-mounted fan. At low speeds, this fan moves less air, potentially causing overheating. For applications requiring frequent low-speed operation, choose a motor with an independent forced cooling fan (TEFC – Totally Enclosed Fan Cooled with separate blower). This ensures consistent cooling regardless of motor speed.
4. Check Certification Standards
Ensure the motor carries relevant certifications for your target market. Common standards include:
| Region/Standard |
Description |
Applicability |
| ATEX |
European Union directive for explosive atmospheres |
Europe, Global recognition |
| IECEx |
International Electrotechnical Commission scheme |
Global, widely accepted |
| NEC / UL |
National Electrical Code (USA) |
North America |
| GB / MA |
Chinese National Standards / Mining Safety |
China, Mining sector |
Common Challenges and Maintenance Best Practices
Even the best-engineered explosion-proof variable frequency motors require proper maintenance to ensure long-term safety and reliability. Ignoring specific maintenance needs can compromise the explosion-proof integrity of the unit.
Thermal Management Issues
One of the most common issues is overheating due to harmonic distortion from the VFD. If the motor runs hot, check the VFD carrier frequency settings. Increasing the carrier frequency can reduce motor noise but may increase heating. Finding the optimal balance is key. Regularly inspect cooling fins and independent fans for dust buildup, which acts as an insulator and traps heat.
Bearing Currents and Failure
VFDs can induce high-frequency circulating currents in the motor bearings, leading to pitting and premature failure. If you notice unusual noise or vibration, inspect the bearings for electrical discharge machining (EDM) damage. Installing shaft grounding brushes or using insulated bearings can mitigate this issue. Regular lubrication with the correct grade of grease is also essential.
Integrity of Explosion-Proof Enclosure
The safety of the motor depends on the integrity of its enclosure. Never modify the housing or drill holes without manufacturer approval. Ensure that all cable entries use certified explosion-proof glands. Regularly inspect flame paths and mating surfaces for corrosion or damage. Any gap larger than specified can allow an internal explosion to propagate to the outside environment.
Frequently Asked Questions (FAQ)
Can I use a standard explosion-proof motor with a VFD?
While physically possible, it is not recommended. Standard explosion-proof motors may not have the insulation strength to handle VFD voltage spikes, leading to early winding failure. Additionally, they may lack adequate cooling at low speeds. Always use a motor specifically rated for inverter duty in hazardous locations.
What is the difference between Ex d and Ex e motors?
Ex d (Flameproof): The enclosure can withstand an internal explosion and prevent it from spreading to the outside. It is robust and suitable for Zone 1 and Zone 2.
Ex e (Increased Safety): Focuses on preventing sparks and high temperatures during normal operation. It is generally lighter and cheaper but typically restricted to Zone 1 for certain components or Zone 2. Ex d is more common for complete motor assemblies in high-risk areas.
How does a VFD affect the explosion-proof rating?
The VFD itself is usually installed in a safe area. If the VFD must be installed in a hazardous area, it must also be housed in an explosion-proof enclosure or be certified as intrinsically safe. The motor’s rating remains unchanged, but the entire system (motor + cable + drive) must be compliant. Long cable runs between the VFD and motor may require output filters to protect the motor insulation.
Why is customized production important for these motors?
Industrial applications vary widely in terms of voltage, frequency, mounting size, and environmental conditions. Off-the-shelf solutions may not fit existing infrastructure or meet specific safety protocols. Customized production allows for tailored shaft dimensions, special coatings for corrosion resistance, and integration with specific control protocols, ensuring seamless operation and compliance.
Conclusion: Ensuring Safety and Efficiency in Hazardous Operations
Investing in a high-quality explosion-proof variable frequency motor is a strategic decision that balances safety, efficiency, and operational control. By enabling precise speed adjustment in hazardous environments, these motors reduce energy costs, extend equipment life, and enhance process stability. However, the complexity of these systems demands a supplier with deep technical expertise and rigorous quality control.
At Zibo Hongcheng Fans, we combine decades of industry experience with modern manufacturing capabilities to deliver ventilation and drive solutions that meet the toughest safety standards. Whether you are upgrading an existing mine ventilation system or designing a new chemical processing plant, our team provides the technical support and customized products you need.
Do not compromise on safety or performance. Contact our engineering team today to discuss your specific application requirements. We are ready to provide detailed technical parameters,选型 advice, and customized solutions to ensure your operations run safely and efficiently.
Explore Our Full Range of Explosion-Proof Fans and Motor Solutions