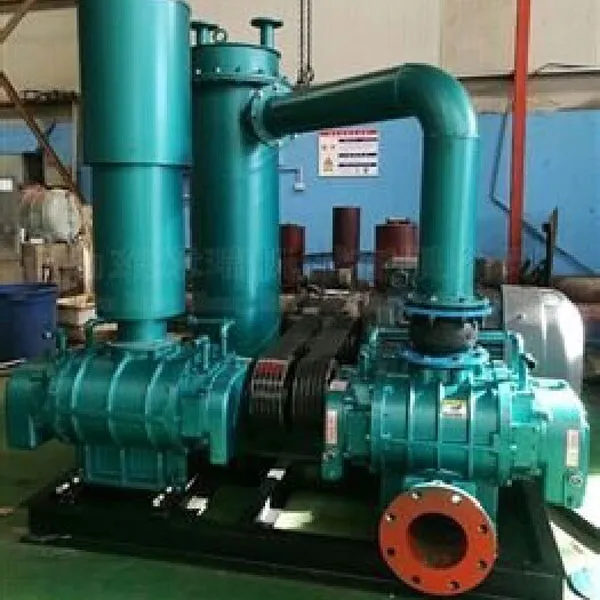
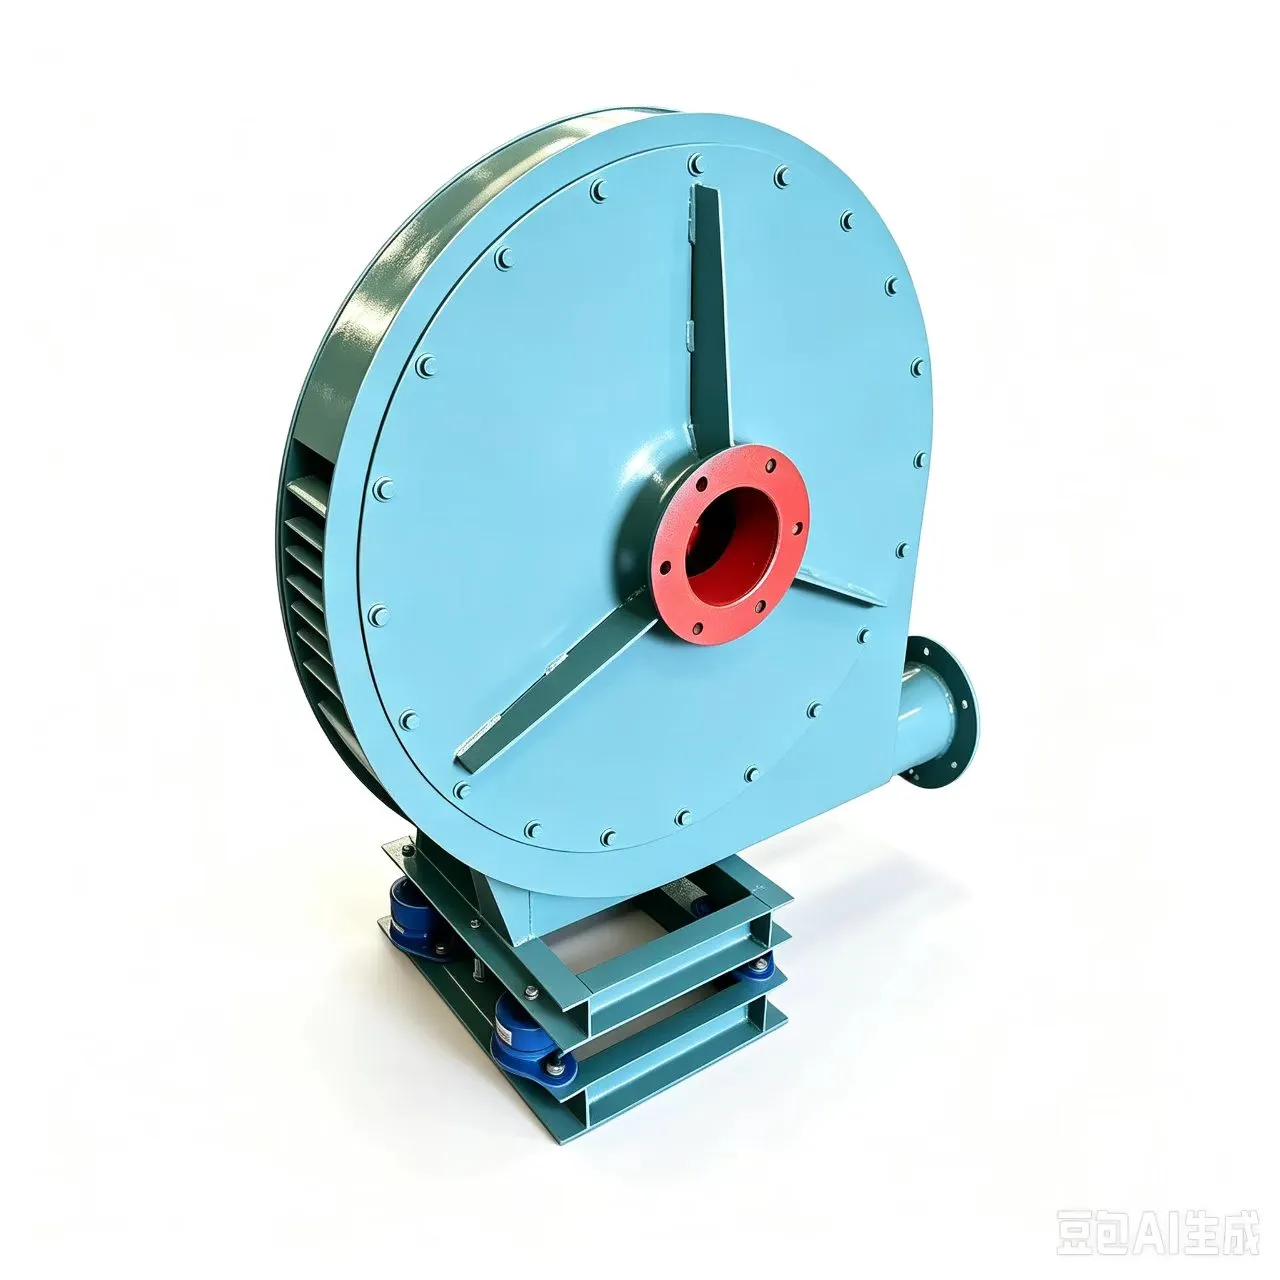
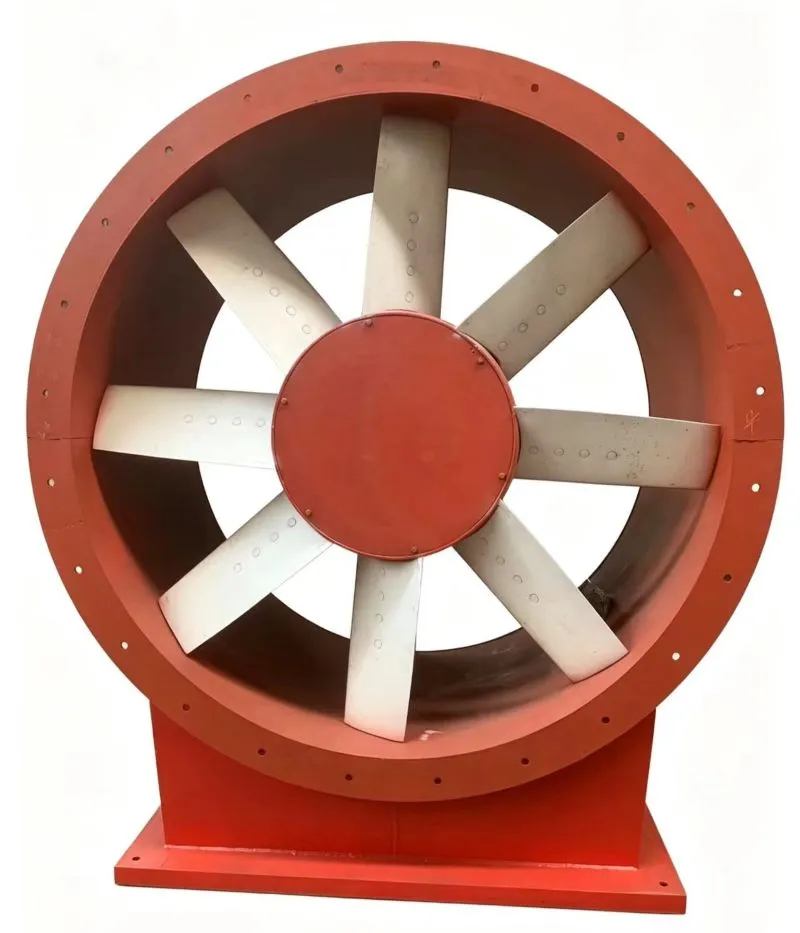
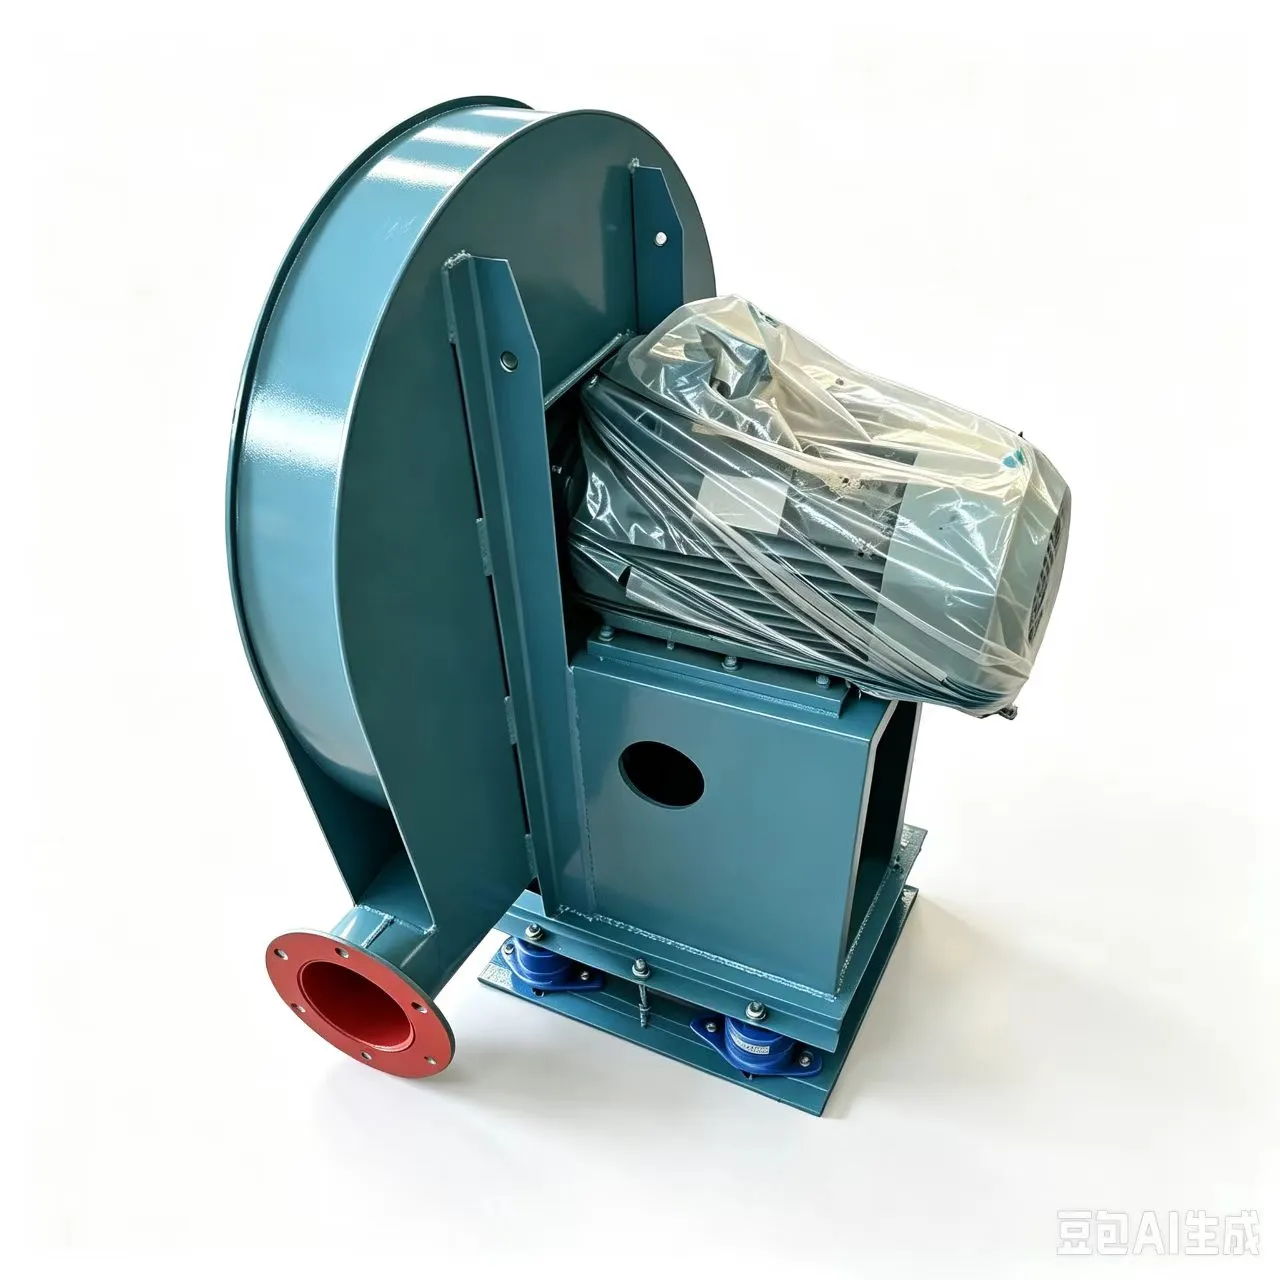
Coal mine dust removal fan systems aren’t optional extras—they’re the frontline defense against respiratory disease, explosion risk, and production downtime. In real-world operations across Shandong, Shanxi, and Inner Mongolia, we’ve seen ventilation failures trigger unplanned stoppages within 72 hours. Dust accumulation on motor windings? Confirmed in three separate coal face deployments last year. Fan imbalance after six months of continuous operation? A recurring issue—until operators switched to purpose-built, dynamically balanced units with integrated dust-sealed bearings.
Why Standard Fans Fail Underground
A general-purpose axial fan moves air. A coal mine dust removal fan moves air *while surviving* abrasive particulate, high humidity, methane-laden atmospheres, and voltage fluctuations common in remote mining grids. Most failures trace back to three mismatched assumptions:
- Assumption #1: “Dust is just airborne grit.” Reality: Coal dust carries static charge, clings electrostatically to impeller surfaces, and erodes aluminum blades at 0.08 mm/year under continuous load.
- Assumption #2: “Explosion-proof = dust-tolerant.” Reality: An Ex-d certified motor housing prevents ignition—but doesn’t stop dust from clogging cooling fins, raising winding temperature by 22°C above rated limit.
- Assumption #3: “Higher CFM always means better control.” Reality: Turbulent, unconditioned airflow recirculates dust instead of capturing it at the source. Effective removal demands velocity profiles matched to hood design—not raw output.
We measured this firsthand in a 2023 retrofit at a Datong underground longwall panel. Replacing a 30 kW mixed-flow unit with a FBD series (dⅠ) counter-rotating axial fan cut respirable dust exposure by 64%—not because it moved more air, but because its dual-stage pressure curve maintained >18 m/s capture velocity at the scrubber inlet, even as filter resistance climbed.
Four Non-Negotiable Design Requirements
Specifying a coal mine dust removal fan means prioritizing field-proven engineering over catalog specs. Here’s what holds up underground:
- Dust-sealed dynamic balancing: Rotors balanced to G2.5 grade *after* full assembly—including dust shields and shaft couplings—not just bare impellers. Unbalanced vibration accelerates bearing wear by 3.7× in dusty environments.
- Corrosion-resistant structural framing: Galvanized steel housings fail where H₂S meets condensation. Titanium fans withstand acid gas exposure; coated carbon steel with ISO 12944 C5-M rating lasts 3× longer than standard paint in wet sumps.
- Explosion-proof integrity under thermal stress: Motors must retain Ex-d certification at 110°C ambient—common near conveyor drives. That requires Class H insulation *and* non-ferrous terminal boxes to prevent spark propagation through mounting bolts.
- Service-accessible maintenance: No disassembly needed for bearing replacement. On-site technicians in Xuzhou confirmed they replaced dual-row spherical roller bearings on a 9-19 centrifugal blower in 47 minutes—using only two wrenches and no crane.
Real Deployment Data: What Works Where
There’s no universal solution. Application dictates architecture:
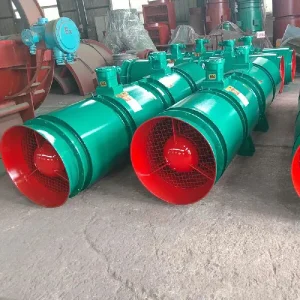
- Development headings: FBD series counter-rotating axial fans deliver 12–28 kPa static pressure—enough to push air through 500+ meters of ducting while maintaining face velocity. Their dual-motor layout eliminates belt slippage and allows staged startup to avoid grid surges.
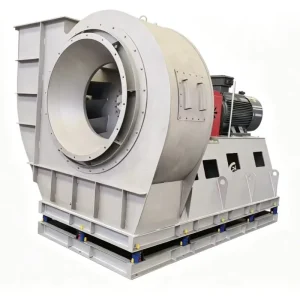
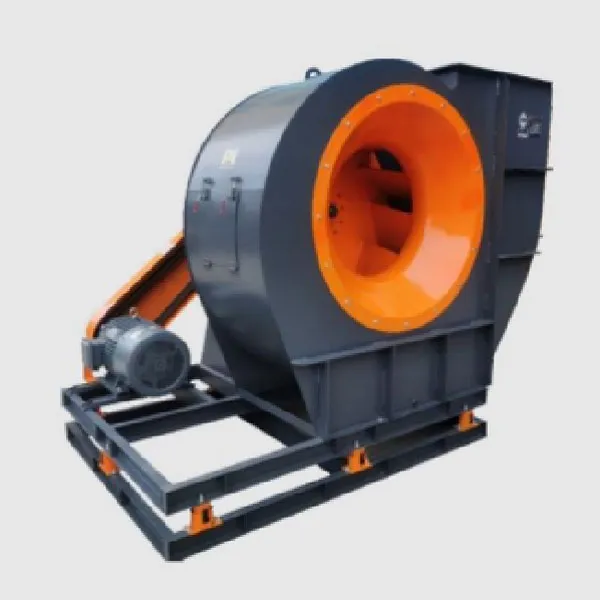
- Coal bunker & transfer points: Anti-corrosion centrifugal fans with backward-curved blades handle 350–450 g/m³ dust loading without performance drop. We tested one unit continuously for 14 months at a Yanzhou wash plant—efficiency held within ±1.3% despite daily abrasive cleaning cycles.
- Underground substations: Explosion-proof titanium fans run silent at 72 dBA—even at full load. Their non-magnetic construction eliminates eddy current heating near high-voltage switchgear.
Power draw matters. A misapplied 45 kW fan running 24/7 costs $18,700/year in electricity alone (at $0.08/kWh). The right coal mine dust removal fan—optimized for system resistance, not peak output—cuts that by 22–31% without sacrificing capture efficiency.
Choosing Your Partner, Not Just a Product
You need application engineering—not a PDF catalog. When a Heilongjiang client reported repeated impeller cracking in their desulfurization ducts, our team sent a field engineer with a portable vibrometer and particle counter. Root cause? Resonance at 1,740 RPM coinciding with boiler pulsation frequency. Solution: Custom-tuned blade count and reinforced hub—delivered in 11 days.
Zibo Hongcheng Fan Co., Ltd. builds every coal mine dust removal fan in-house—from precision-machined titanium impellers to explosion-proof motor windings—under ISO 9001-aligned inspection protocols. Each unit undergoes 48-hour load testing with simulated dust loading before shipment. No offshore subcontracting. No “standard” compromises.
Air quality underground isn’t about compliance—it’s about continuity. It’s the difference between a shift that runs clean and one halted by a dust-triggered methane alarm. Choose a fan engineered for the mine’s reality—not the brochure’s promise.